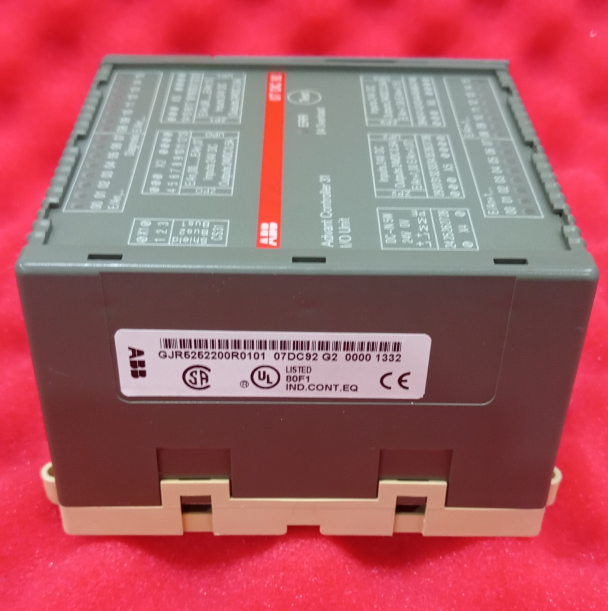
Distributed Control System (DCS) maintenance carries high operational stakes. A single point of failure in I/O hardware triggers cascading process downtime, leading to severe production losses and safety hazards. Maintaining legacy infrastructure or expanding industrial systems introduces complex engineering challenges. Plant engineers must match existing infrastructure with correct replacement components without causing configuration conflicts or system faults. Selecting the wrong hardware results in communication errors, software mismatches, or physical space constraints within control cabinets.
A structured evaluation framework helps you select the appropriate ABB 800xA I/O Module. This process requires strict attention to firmware compatibility, redundancy requirements, lifecycle management, and operator effectiveness. Plant personnel evaluate physical constraints alongside logical configuration needs. Proper selection ensures system uptime, maintains process stability, and simplifies future maintenance interventions across the plant floor.
Selecting the correct ABB 800xA I/O Module requires verifying firmware compatibility with existing AC 800M controllers to prevent communication faults.
High-availability processes demand modules that support seamless redundancy and hot-swapping capabilities to ensure zero-downtime maintenance.
Physical footprint and cabinet constraints dictate the choice between standard S800 I/O and compact S800L series modules.
Proper configuration via Plant Explorer and Control Builder is as critical as hardware selection for ensuring operator effectiveness and system stability.
Table of Contents
Toggle
ABB 800xA I/O Module System Overview
The I/O module serves as the physical bridge within the ABB Ability™ System 800xA® architecture. Field devices like pressure transmitters, temperature sensors, and control valves generate or receive raw analog and digital signals. These signals require precise conversion for the control system to process them. The I/O hardware digitizes field data for the AC 800M controller and converts controller commands back into physical actions. This bidirectional flow forms the operational foundation of any distributed control system.
S800 vs. S800L I/O Series
The standard S800 I/O line offers extensive modularity. It supports a wide range of signal types and complex process control requirements. Engineers deploy standard S800 modules when redundancy is mandatory. These modules mount on distinct Module Termination Units (MTUs), such as the TU810 or TU830. This separation allows for advanced wiring configurations and module replacement under power without disturbing the field wiring.
The compact S800L I/O series provides a different engineering approach. It targets scenarios requiring a smaller physical footprint. S800L modules integrate the I/O circuitry and the terminal block into a single unit. This design saves cabinet space but sacrifices redundancy capabilities and hot-swap functionality. Engineers specify the S800L for non-redundant, space-constrained applications where process interruptions during maintenance are acceptable.
When deciding between the two series, field engineers typically follow a specific evaluation sequence:
Measure the available DIN rail space inside the existing control cabinet.
Identify the redundancy requirements for the specific control loop.
Determine if the process allows for a localized power-down during future module replacements.
Assess the need for advanced channel-level diagnostics or HART communication.
Review the environmental conditions to determine if conformal coating is necessary.
Technical Feature
Standard S800 I/O
Compact S800L I/O
Hardware Modularity
High (Separate electronic module and MTU)
Low (Integrated module and terminals)
Redundancy Support
Yes (Full hardware redundancy via dual MTUs)
No (Single configuration only)
Hot-Swapping
Supported (Replace under live power)
Not Supported (Requires cluster power down)
Physical Footprint
Standard cabinet requirements (e.g., 800mm width)
Highly compact, space-saving design
HART Communication
Supported on specific modules (e.g., AI845)
Limited support depending on module type
Integration with AC 800M Controllers and HMIs
Communication pathways dictate how hardware interacts across the plant. I/O modules interface with the AC 800M controller via specific industrial protocols. Local clusters typically utilize the electrical ModuleBus, which supports up to 12 modules per cluster. For extended distances, the optical ModuleBus uses TB820V2 optical cluster modems to connect remote racks. Remote I/O drops rely on fieldbus protocols like Profibus DP or PROFINET, extending the control architecture across vast plant floors.
This hardware acts as a foundational element in the extended automation context. It links raw field data directly to Human-Machine Interfaces (HMIs), creating a unified operator environment. Hardware choices directly impact the logical configuration within the Plant Explorer environment. The physical hardware tree built in the cabinet must perfectly match the logical software tree built in the engineering station. Any discrepancy between the physical module type and the Plant Explorer configuration triggers immediate system faults and prevents the controller from entering run mode.
Goals for DCS Maintenance Work
Establishing baseline requirements is mandatory before initiating any maintenance intervention or system expansion. Engineers must define what constitutes a successful upgrade. Success means restoring full functionality without introducing new failure points. It requires matching legacy constraints with modern performance standards while keeping the process running.
Minimizing Process Downtime
ABB S800 I/O modules can support hot-swapping in compatible configurations, allowing qualified technicians to replace faulty modules without disconnecting field wiring. The Module Termination Unit (MTU) simplifies replacement and reduces wiring errors. These features help shorten Mean Time to Repair (MTTR), minimize maintenance downtime, and improve system availability in continuous industrial processes.
Legacy Compatibility and Lifecycle Status
Industrial control systems operate for decades, but electronic hardware lifecycles do not. ABB manages products through four distinct lifecycle phases. Plant managers must audit current inventory against available replacement modules. Installing an Obsolete module into a critical control loop introduces unacceptable risk. Engineers target Active or Classic modules for all maintenance activities to ensure long-term support.
Lifecycle Phase
Definition and Support Level
Engineering Action Required
Active
Product is in active sales and manufacturing. Full support available.
Standardize on these modules for new expansions.
Classic
Product is no longer actively promoted but fully supported with spares.
Acceptable for direct replacements in existing racks.
Limited
Spare parts are scarce. Support is limited to existing inventory.
Plan migration strategy. Do not use for new loops.
Obsolete
Product is no longer manufactured or supported.
Immediate upgrade required to prevent extended downtime.
Consulting official technical documentation is non-negotiable. Engineers reference ABB data sheets and maintenance manuals to verify exact specifications for Analog Input (AI), Analog Output (AO), Digital Input (DI), and Digital Output (DO) modules before procurement. Guessing signal ranges or isolation levels leads to equipment damage and blown fuses.
Firmware and software matching represents a critical validation step. Hardware does not operate independently. You verify that the new module's firmware is supported by the existing version of Control Builder. A newer module might require a software patch or a complete controller firmware upgrade. Failing to check this compatibility results in modules that power up but refuse to communicate on the ModuleBus.
Key Factors to Select ABB 800xA I/O Modules
Mapping specific technical specifications to operational outcomes ensures reliability. Every hardware feature serves a maintenance or control objective. Engineers evaluate modules across several strict dimensions to guarantee system stability and process safety.
Signal Types and Channel Density
ABB S800 I/O module selection depends on signal type, voltage compatibility, and channel requirements. Modules support different analog and digital signals, including 4–20 mA, RTDs, thermocouples, and discrete inputs. High-density modules save cabinet space, while lower-density configurations can reduce the number of signals affected by a single module failure.
Redundancy and High-Availability Requirements
Redundant I/O configurations improve system availability in critical industrial processes. Compatible modules, termination units, communication interfaces, and power supplies can provide fault tolerance and support continuity during certain hardware failures. Redundancy design should match the application's reliability requirements and supported ABB system architecture.
Diagnostic Capabilities and Operator Visibility
Advanced I/O diagnostics help operators identify signal abnormalities, wiring faults, and module failures through the ABB System 800xA interface. Features such as channel-level monitoring, wire-break detection, and fault alarms simplify troubleshooting, reduce maintenance time, and improve process reliability.
Communication Interfaces and Fieldbus Protocols
Communication interface selection depends on network compatibility, fieldbus protocols, and control response requirements. ABB systems may use interfaces such as CI854 for PROFIBUS DP and CI871 for PROFINET. Proper network configuration and load management help maintain stable communication between controllers and field devices.
Financial and Operational Trade-Offs
ABB I/O module selection should consider initial hardware costs, reliability, cabinet space, maintenance requirements, and long-term spare parts availability. Balancing these factors helps optimize system lifecycle costs.
Upfront Hardware Costs vs. Long-Term Reliability
Standard I/O modules provide essential signal processing at lower initial costs, while advanced variants may offer enhanced diagnostics or environmental protection. Selecting compatible, reliable modules and standardizing spare parts can reduce maintenance complexity, replacement costs, and long-term downtime.
Footprint and Cabinet Space Constraints
Cabinet space and thermal management are important considerations when expanding ABB S800 I/O systems. Compact or high-density modules help reduce installation space, but increased component density may affect heat dissipation. Proper cabinet layout, ventilation, and temperature monitoring support reliable long-term operation.
Conclusion
Choosing the correct replacement hardware requires balancing physical constraints against operational demands. Redundancy needs, strict firmware compatibility, and operator visibility requirements dictate the final selection. A successful upgrade restores functionality while enhancing long-term system stability and reducing future maintenance overhead.
The shortlisting logic follows a strict sequence. You audit existing hardware and controller firmware. You define the exact signal and redundancy requirements for the specific loops. You consult official data sheets to verify electrical specifications. Finally, you select between the standard S800 and compact S800L series based on cabinet footprint and process criticality.
Audit your current AC 800M controller firmware version before ordering any replacement hardware.
Document the exact signal types and redundancy needs for your field devices.
Calculate the available cabinet space and thermal load for the new modules.
Verify the lifecycle status of your existing modules to plan future migrations.
Consult official ABB hardware manuals for exact wiring diagrams and mechanical keying instructions.
FAQ
Q: What is the difference between ABB S800 and S800L I/O modules?
A: The standard S800 series offers high modularity, full redundancy support, and hot-swapping capabilities for complex processes. It uses separate electronic modules and termination units. The S800L is a compact, cost-effective series with integrated terminals. It requires less cabinet space but does not support redundancy or live replacement under power.
Q: Can I hot-swap an ABB 800xA I/O Module without stopping the process?
A: Yes, standard S800 modules support hot-swapping. You can remove and replace them under live power without disrupting the active control loop. The termination unit maintains the field wiring connections. However, compact S800L modules do not support hot-swapping and require powering down the specific cluster before replacement.
Q: How do I check firmware compatibility for a replacement ABB I/O module?
A: You cross-reference the new module's release notes with your installed AC 800M controller version. Check the hardware library version in Control Builder. If the new module requires a newer library, you must update the controller firmware and the engineering software before the module will communicate on the bus.
Q: What software is used to configure ABB 800xA I/O Modules?
A: Configuration occurs within the System 800xA environment using two primary tools. Plant Explorer builds the logical hardware tree and maps the physical modules to the system. Control Builder sets specific channel parameters, defines signal ranges, adjusts filter times, and writes the actual control logic for the process.
Q: How do I address a ModuleBus communication error on an S800 I/O cluster?
A: First, verify that the module is firmly seated and locked into its termination unit. Next, check the optical cables connecting the clusters for sharp bends or physical damage. Finally, ensure the terminating resistor is correctly installed at the end of the electrical ModuleBus segment on the last MTU.
Q: Are ABB 800xA I/O Modules suitable for hazardous areas?
A: Yes, ABB offers specific intrinsically safe (IS) S800 I/O modules designed for hazardous environments. These modules include built-in barriers to limit electrical energy to field devices. You verify the module carries the appropriate ATEX, IECEx, or UL certifications for your specific hazardous zone classification before installation.
Q: Where can I find exact specifications for analog and digital ABB I/O modules?
A: Detailed parameters for AI, AO, DI, and DO modules reside in official ABB S800 I/O data sheets and hardware maintenance manuals. These documents provide critical engineering data on signal ranges, isolation voltages, power consumption, heat dissipation, and channel-level diagnostic capabilities required for system design.